A finished roll of performance fabric passes through more stages than most product developers realize — and every one of those stages is a point where quality can be gained or lost. Understanding the full sequence, from raw yarn to finished textile, is what lets a buyer ask the right questions during a factory audit instead of just inspecting the final swatch.
This walkthrough follows performance fabric through each production stage, and flags where in that sequence the functional properties brands care about — stretch, moisture management, durability — actually get built in.
Key Takeaways
- Performance fabric passes through five broad stages: yarn preparation, knitting, dyeing, finishing, and quality inspection — each stage can add or compromise functional performance.
- Factories operating under ISO 9001 quality management structure these stages with documented checkpoints, which is why certification status is a legitimate question to ask a new supplier.
- Knit construction — covered in knit vs. woven fabric for sportswear — is set at the knitting stage and can’t be corrected later in finishing.
- Finishing is where topical functional treatments are applied, and it’s also the stage most prone to inconsistency between production batches if not tightly controlled.
Stage 1: Yarn Preparation
Before any knitting happens, raw fiber — whether polyester, nylon, cotton, or a blend — is spun or textured into yarn. This is also where elastane filaments get combined with the base yarn for stretch, and where any wicking-oriented yarn engineering (like multi-channel filament cross-sections) is built in. Fiber choice at this stage has a major downstream effect on comfort and performance; our comparison of polyester vs. cotton for activewear covers how the two most common options diverge from this very first stage onward.
Stage 2: Knitting
Yarn is fed into circular or flat knitting machines that form it into interlocking loops at a specified gauge (needle density). This stage determines the base construction — single jersey, interlock, double knit — and locks in the fabric’s inherent stretch behavior and weight range before dyeing even begins. Construction choices made here can’t be corrected downstream, which is why gauge and construction should be confirmed before committing to bulk production, not after receiving finished yardage.
Stage 3: Dyeing
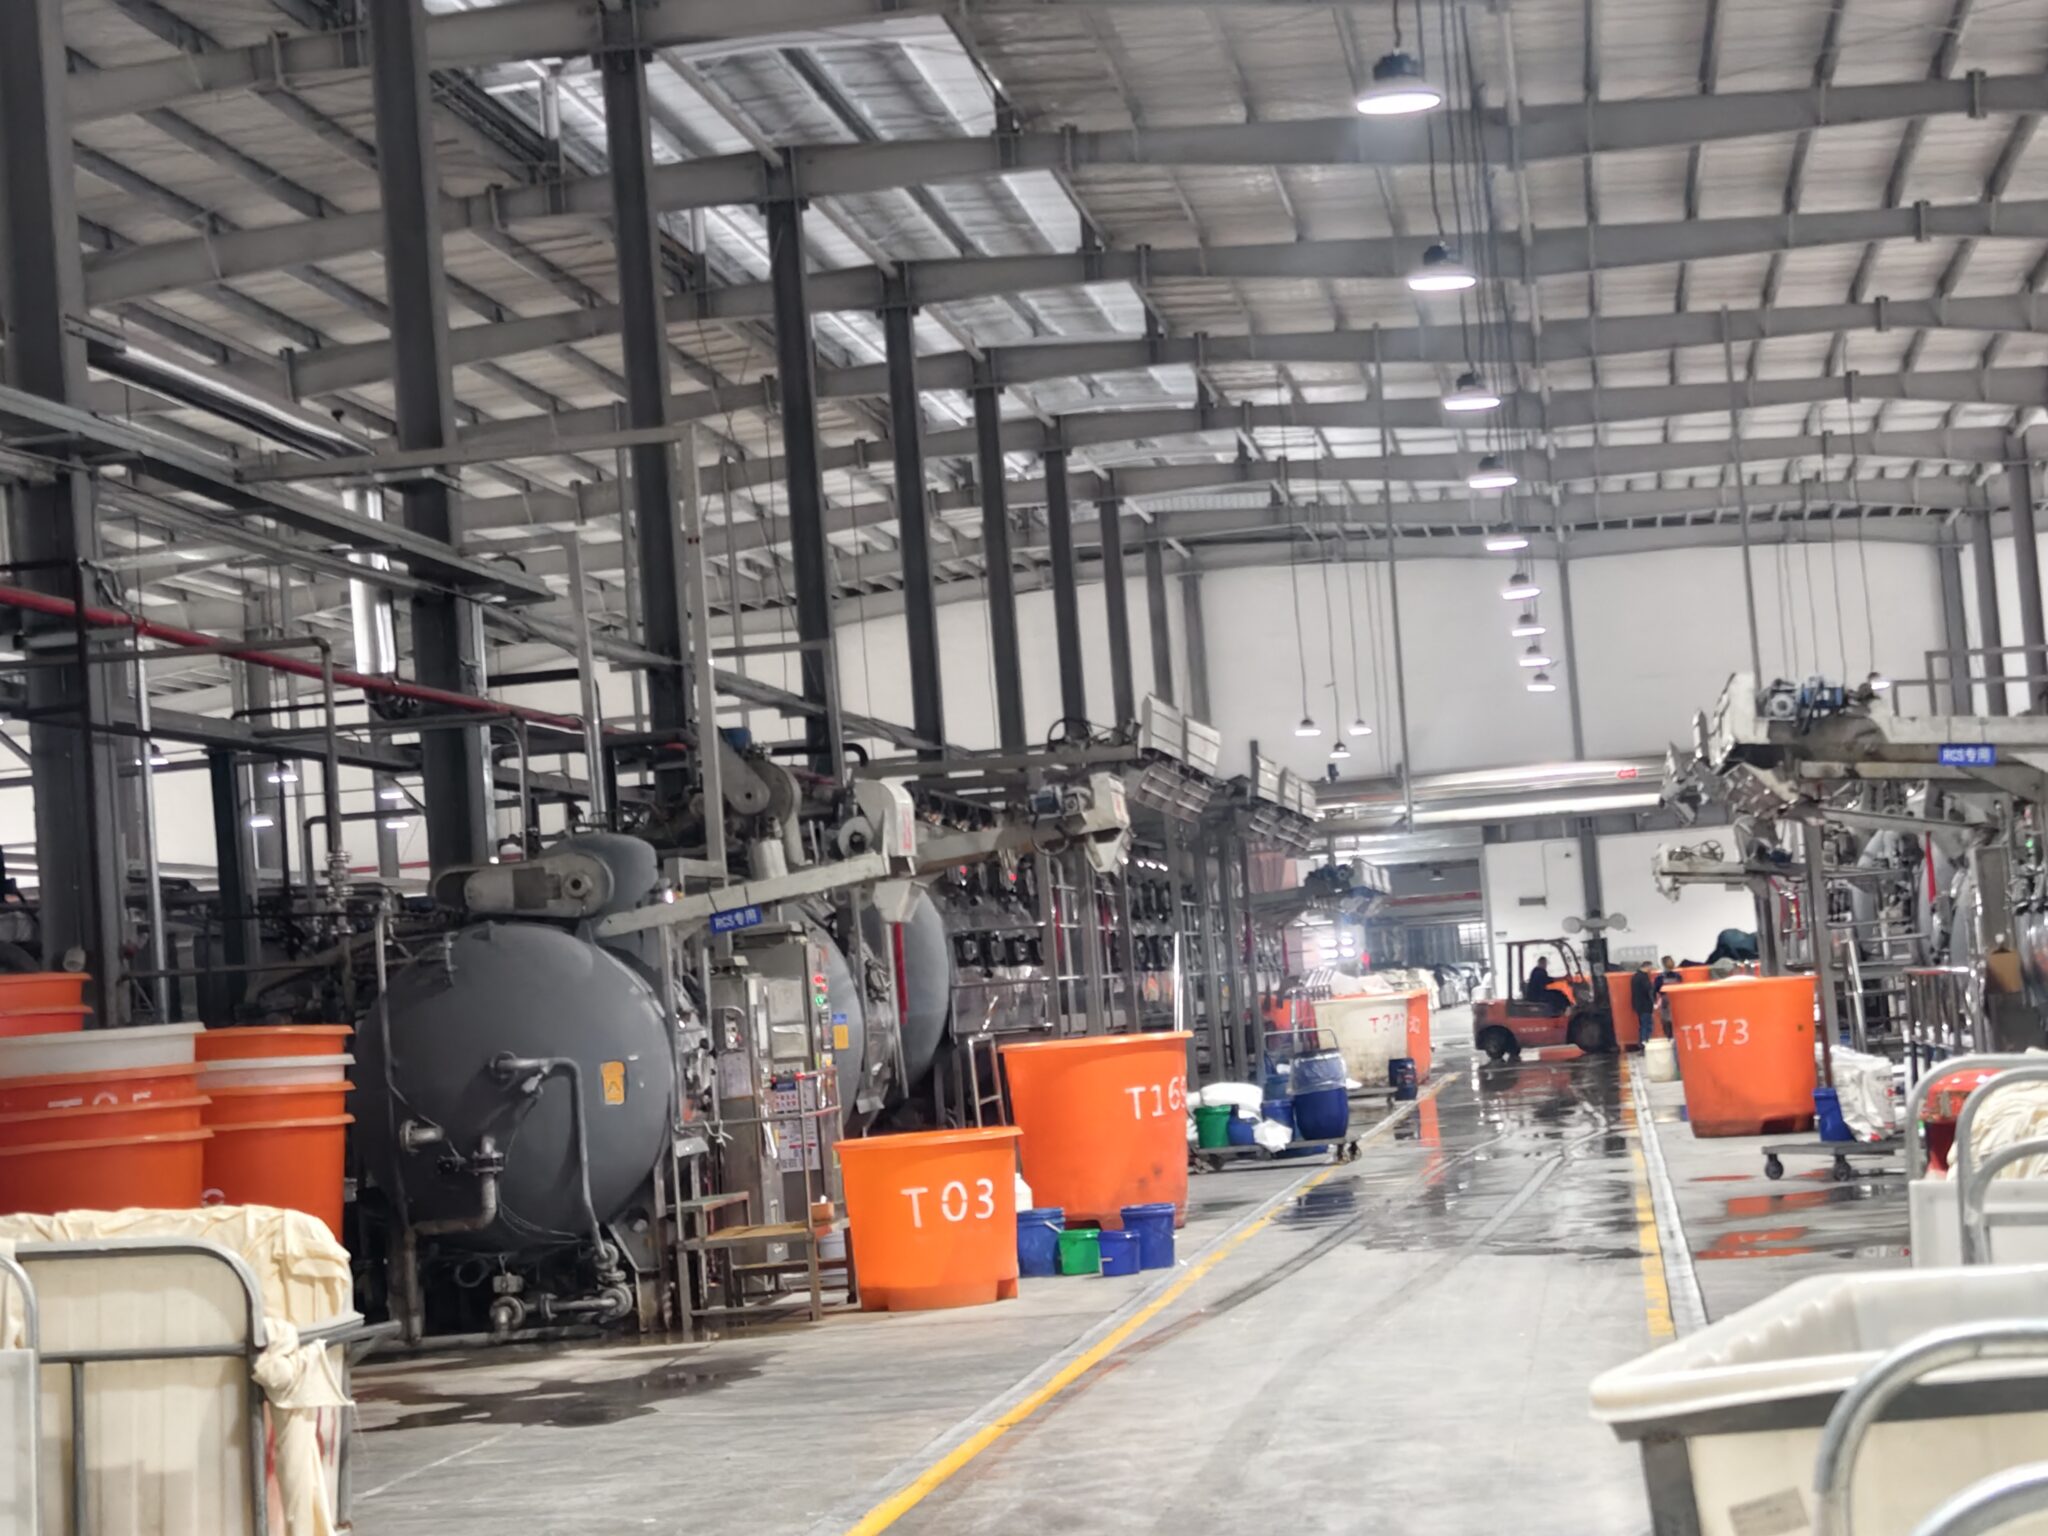
Greige (undyed) fabric is dyed to the brand’s specified color, typically using processes matched to the fiber type — reactive dyes for cotton, disperse dyes for polyester. Dyeing also exposes any structural weaknesses in the knit: poorly constructed fabric can distort or shrink unevenly under the heat and tension of dyeing equipment, which is one reason a pilot dye lot is worth running before a full production batch.
Stage 4: Finishing
This is where topical functional treatments — water repellency, anti-static coatings, odor control — are applied to the dyed fabric. Finishing is also where a fabric’s hand-feel gets its final character, through processes like brushing, calendaring, or heat-setting. Because most functional finishes are applied rather than built into the fiber itself, their durability through repeated washing varies significantly by finish type; our breakdown of the 5 most common performance fabric finishes covers which hold up long-term.
Stage 5: Quality Inspection and Testing
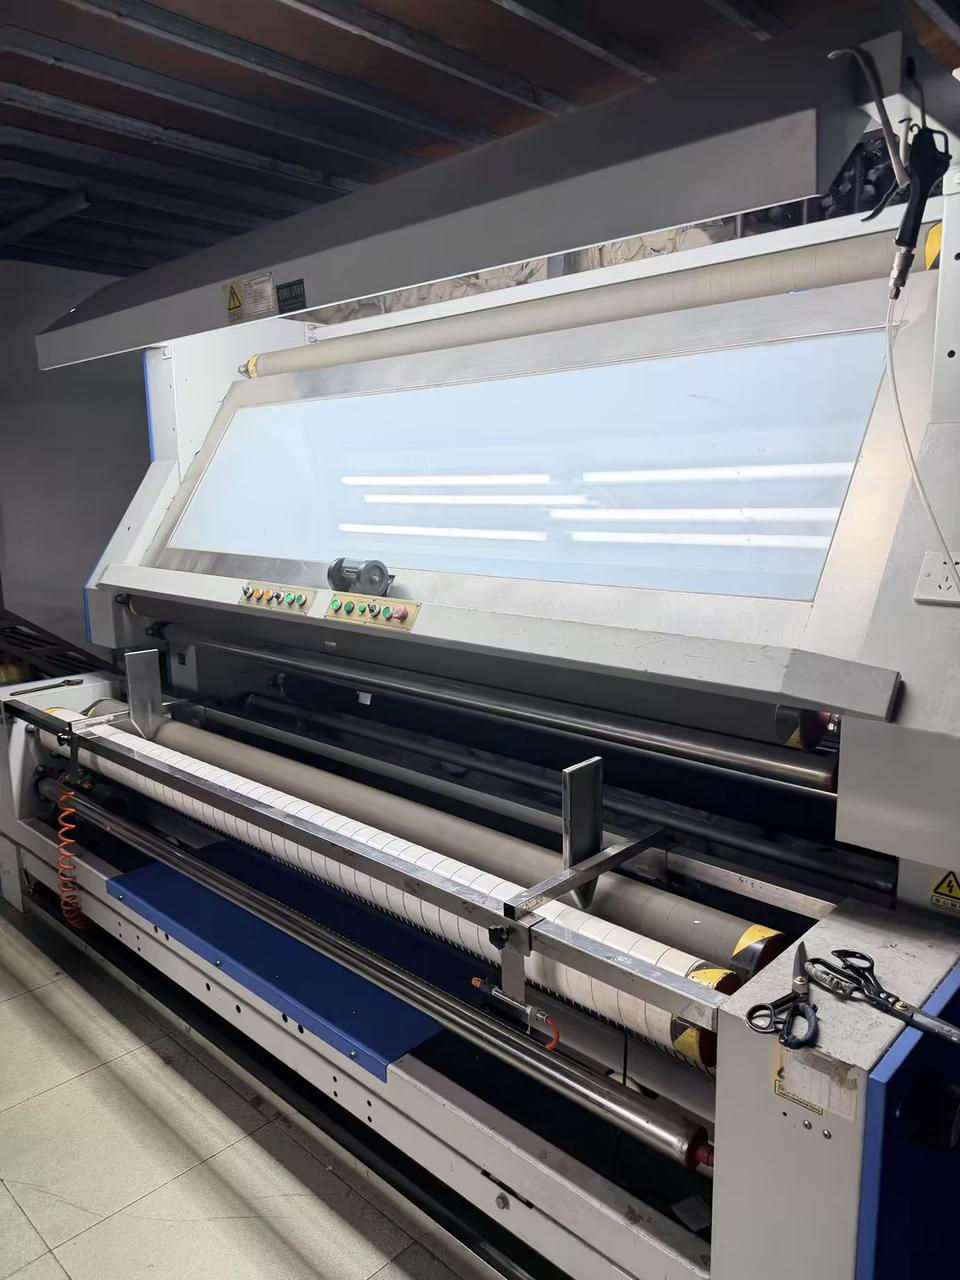
Before fabric ships, it’s checked against the specification — weight (GSM), width, colorfastness, and any functional test the brand has specified (moisture management, stretch recovery, pilling resistance). This is the stage where a fabric’s actual GSM gets verified against what was ordered; see the beginner’s guide to fabric GSM for what that measurement means and why it’s worth spot-checking on incoming shipments rather than trusting the spec sheet alone.
Frequently Asked Questions
Which production stage matters most for moisture-wicking performance?
Yarn preparation and knit structure matter most — moisture management is largely a function of fiber choice and capillary channels built into the yarn, not something finishing can add after the fact. See what is moisture-wicking fabric and how does it work for the mechanism in detail.
Can a factory fix a construction problem during finishing?
No. Finishing can add surface treatments and improve hand-feel, but it can’t correct a knit construction issue like incorrect gauge or loop density — those are set permanently at the knitting stage.
What should I ask a new fabric supplier about their production process?
Ask which stages happen in-house versus outsourced (yarn, knitting, dyeing, and finishing are sometimes split across different facilities), what quality checkpoints exist between stages, and whether they hold ISO 9001 or equivalent certification.
Mibein · Global Brand of Xianwei Textile
Looking for a Reliable Fabric Partner for Your Next Collection?
Mibein is a vertically integrated fabric manufacturer with 20+ years of experience, serving apparel brands worldwide from our own facilities in Guangzhou. Tell us what you’re working on and we’ll help you find the right fabric.
Ready color cards · Meter samples · Flexible MOQ for new product programs
Sources: ISO 9001 Quality Management